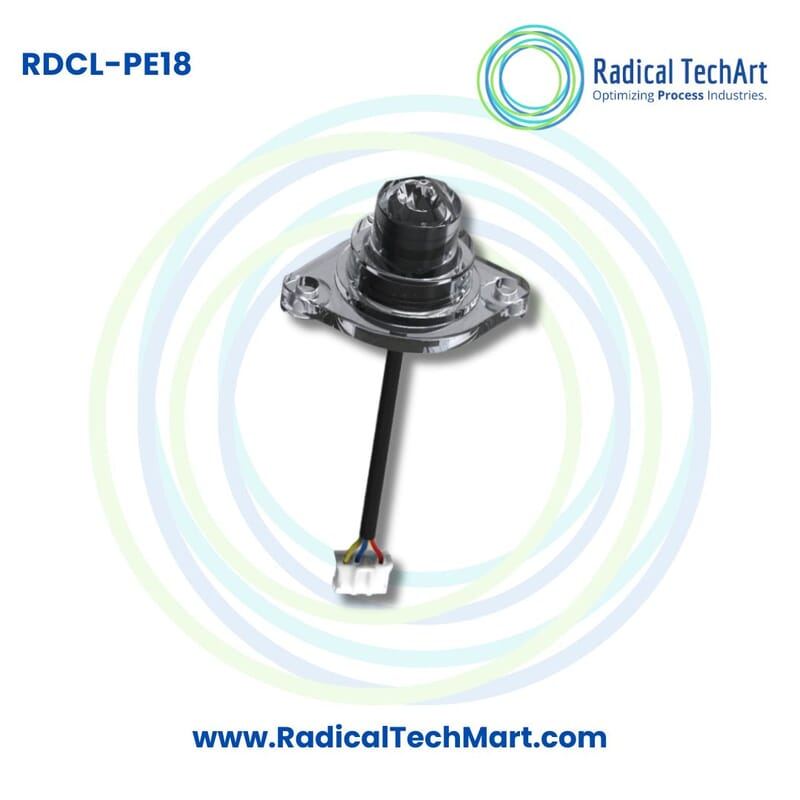
RDCL Infrared Liquid Level Switch RDCLPE18
The RDCL Infrared Liquid Level Switch RDCLPE18 is a compact photoelectric liquid level sensor designed for fast and accurate water level detection in tanks, appliances, and automated equipment. It uses infrared light reflection and refraction technology to detect the presence or absence of liquid without mechanical moving parts. Operating on a 5V DC power supply with a temperature range of -25°C to 85°C, the RDCLPE18 offers high repeatability, reliable switching, and low maintenance. It is ideal for coffee machines, water dispensers, humidifiers, robotic vacuum cleaners, steam appliances, and industrial liquid level control applications.
Customize
Share :
A. Product Overview
The RDCL RDCLPE18 Infrared Liquid Level Switch is a compact photoelectric sensor that detects liquid presence at a fixed point in a tank or container. It distinguishes air from liquid through changes in infrared light reflection and refraction at its sensing surface.
Unlike mechanical float switches, the RDCLPE18 has no moving sensing parts. Its fast, repeatable electronic detection supports high-level and low-level alarms, water shortage protection, overflow prevention and automatic replenishment.
It suits appliances, robotic cleaning equipment, water dispensers and automated liquid handling systems.
Important Technical Specifications
| Specification | Details |
|---|---|
| Product Name | Infrared Liquid Level Switch |
| Brand | RDCL |
| Model Number | RDCLPE18 |
| Sensor Type | Infrared Photoelectric Liquid Level Sensor |
| Detection Principle | Infrared Light Reflection and Refraction |
| Infrared Wavelength | Approximately 850 to 950 nm |
| Operating Voltage | 5V DC |
| Output When Water Is Present | 0V Typical |
| Output When Water Is Absent | 5V Typical |
| Current Consumption, Water Present | 15 mA Typical |
| Current Consumption, Water Absent | 20 mA Typical |
| Operating Temperature | -25°C to 85°C |
| Detection Method | Point Level Detection |
| Response Characteristics | Fast Response |
| Repeatability | High Repeatability |
| Mechanical Moving Parts | None |
| Typical Applications | Water Level Detection, Overflow Prevention, Water Shortage Protection |
Note: Electrical values are typical at 5V DC and 25°C. Confirm the unspecified response time, dimensions and output configuration before installation.
B. Working Principle
The RDCLPE18 uses infrared photoelectric sensing. An emitter directs light toward a sensing surface while a receiver monitors reflections.
When the surface is surrounded by air, light follows a particular reflection path. When water reaches the surface, the refractive-index difference changes the reflected light intensity. The circuit interprets this change as wet or dry and switches its output.
Step-by-Step Working Process
- Infrared Light Emission: The sensor produces near-infrared light, typically around 850 to 950 nm.
- Dry Condition Detection: With air around the sensing surface, reflected light produces a reference signal at the receiver.
- Liquid Contact Detection: Contact with liquid changes light reflection and refraction due to its different refractive index.
- Optical Signal Detection: The receiver detects the change in reflected light intensity.
- Electrical Signal Generation: The circuitry switches its electrical output based on whether liquid is present.
- Automatic Level Control: A compatible controller can trigger alarms, stop heating, prevent dry running or activate replenishment.
Typical Output Conditions
| Detection Condition | Typical Output Voltage |
|---|---|
| Water Present | 0V |
| Water Absent | 5V |
These values apply at a 5V DC supply and 25°C.
Important: RDCLPE18 is a point level switch, not a continuous level transmitter. It detects liquid at the installed sensing position rather than measuring the full height or volume of liquid in the tank.
C. Why Is the RDCLPE18 Infrared Liquid Level Switch Used?
The RDCLPE18 detects liquid presence in compact equipment, storage containers and automated systems.
1. Accurate Water Level Detection
Its optical sensing principle provides fast, repeatable identification of liquid at a selected tank position, enabling full or empty indication.
2. Water Shortage Protection
In coffee machines, steam cookers, humidifiers and dispensers, low water can damage components. A low-mounted RDCLPE18 can signal a controller to stop operation or issue a refill alert.
3. Prevention of Tank Overflow
Mounted near the maximum filling level, the sensor can signal a connected controller to stop filling or activate an overflow alarm. This is useful in robotic floor cleaners and wastewater collection tanks.
4. Fast Response for Automated Equipment
Infrared detection enables prompt switching as the sensing surface changes between wet and dry conditions, supporting timely automated control.
5. No Mechanical Moving Parts
Unlike float switches, the RDCLPE18 has no floating or rotating sensing mechanisms, reducing mechanical wear during operation.
6. Compact Design for Appliance Integration
Its electronic optical sensing design fits compact equipment such as capsule coffee machines, robotic vacuum cleaners, aroma diffusers and water dispensing systems.
7. High and Low Liquid Level Monitoring
High or low installation enables tank-full detection, low-water warnings and controlled refilling.
8. Reduced Maintenance Requirements
No moving parts reduce mechanical maintenance. Keep the optical surface clean for reliable detection.
D. Suitable Buyers and Industrial Applications
The RDCLPE18 suits OEMs, equipment designers and automation companies needing compact point level detection.
| Suitable Buyers | Typical Applications |
|---|---|
| Coffee Machine Manufacturers | Low-water detection and dry-heating prevention |
| Capsule Coffee Machine Manufacturers | Water shortage alarms and refill indication |
| Robotic Vacuum Cleaner Manufacturers | Clean and dirty water tank monitoring |
| Floor Cleaning Machine Manufacturers | Wastewater tank overflow detection |
| Humidifier Manufacturers | Low-water automatic shutdown |
| Aroma Diffuser Manufacturers | Water shortage detection and atomizer protection |
| Steam Cooker Manufacturers | Water monitoring during steam generation |
| Garment Steamer Manufacturers | Low-water and heating protection |
| Steam Mop Manufacturers | Water shortage monitoring |
| Smart Toilet Manufacturers | Water tank monitoring and inlet valve control |
| Water Dispenser Manufacturers | Low-water alarms and hot-water tank monitoring |
| Tea Machine Manufacturers | Water level monitoring and automatic filling |
| OEM Equipment Manufacturers | Compact electronic point level detection |
| Industrial Automation Companies | Compatible liquid level control system integration |
Common Applications
- Coffee machine and capsule coffee machine water shortage detection
- Robotic vacuum cleaner clean-water tank monitoring
- Floor washer dirty-water tank monitoring and overflow alarms
- Humidifier and aroma diffuser low-water protection
- Steam cooker, garment steamer and steam mop water monitoring
- Smart toilet water tank control
- Water dispenser and tea machine level control
- High-level and low-level water alarms
- Automatic water replenishment systems
- Compact liquid tank level detection
E. Frequently Asked Questions (FAQ)
1. What is the RDCL RDCLPE18 Infrared Liquid Level Switch?
The RDCLPE18 is a compact infrared photoelectric sensor designed to identify whether liquid is present at a fixed position inside a tank or container.
It operates on a typical 5V DC supply and provides an electrical signal for liquid level monitoring, alarms and automatic control.
2. How does the RDCLPE18 Infrared Liquid Level Switch work?
The sensor directs infrared light toward an optical sensing surface. When water contacts this surface, the difference between the refractive indices of air and liquid changes the amount of reflected light.
An internal photoelectric receiver detects this variation, and the electronics generate the corresponding switching output.
3. What is the operating voltage of the RDCLPE18?
The RDCLPE18 operates on a typical 5V DC power supply. Electrical connection details should be checked for the selected version before installation.
4. What is the operating temperature range of the RDCLPE18?
The specified operating temperature range is -25°C to 85°C. The actual installation should remain within the sensor's stated operating conditions.
5. What is the output voltage when water is present?
Under the stated 5V DC supply and 25°C test conditions, the typical output is 0V when water contacts the sensing surface.
6. What is the output voltage when water is absent?
When the sensing surface is not in contact with water, the typical output is 5V under the same specified test conditions.
7. Can the RDCLPE18 be used in coffee machines?
Yes. The RDCLPE18 can detect low-water conditions in coffee and capsule coffee machines. A connected controller can use its signal to stop heating, prevent dry operation or alert the user to refill the tank.
8. Is the RDCLPE18 suitable for robotic vacuum cleaners?
Yes. It can monitor selected levels in the clean-water and dirty-water tanks of compatible robotic vacuum cleaners and floor washing equipment.
9. Can the RDCLPE18 prevent a water tank from overflowing?
The sensor can detect when water reaches an installed high-level position. A compatible controller can then stop filling or activate an overflow warning. A separate control circuit operates the filling equipment.
10. Can the RDCLPE18 be used in humidifiers?
Yes. It is suitable for low-water detection in compatible humidifiers, aroma diffusers and atomizers. The output can be used to shut down equipment when water drops below the sensing point.
11. Does the RDCLPE18 have any mechanical moving parts?
No. It detects liquid optically using infrared light and a photoelectric receiver, without a moving float or mechanical sensing mechanism.
12. What is the current consumption of the RDCLPE18?
Typical current consumption is approximately 15 mA with water present and 20 mA with water absent, measured at 5V DC and 25°C.
13. What wavelength does the RDCLPE18 use for liquid detection?
The sensor uses near-infrared light. The available product information specifies a typical wavelength range of approximately 850 to 950 nm.